Extensive drainage
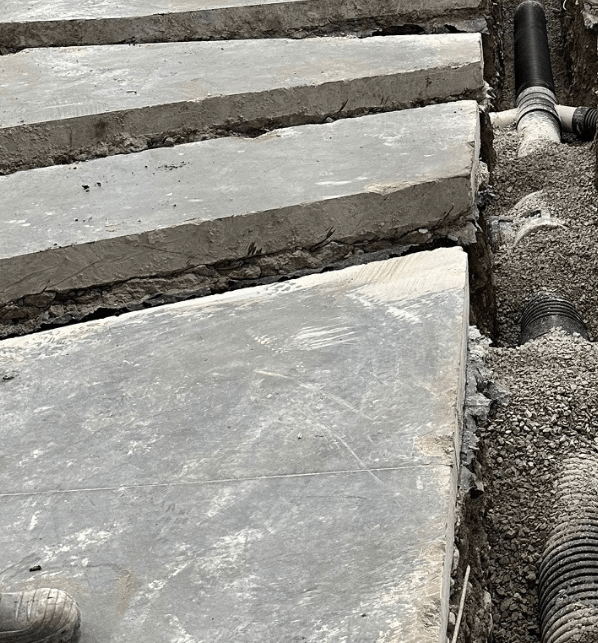
Stockton installed a comprehensive internal and external drainage network to manage foul water and stormwater. This included embedding stainless-steel linear channels to continuously catch water. These were chosen for their corrosion-resistant and durable qualities – important for the hygienic environment food processing requires.
Stockton also installed gullies to collect water run-off before it accumulates and prevent sewer gases escaping into the open air or inside the building. The team constructed manhole chambers to allow safe access to the pipe network for maintenance engineers to complete routine inspections and built a pumping station to lift collected water upward and on toward the nearest sewer line.

Structural and external works
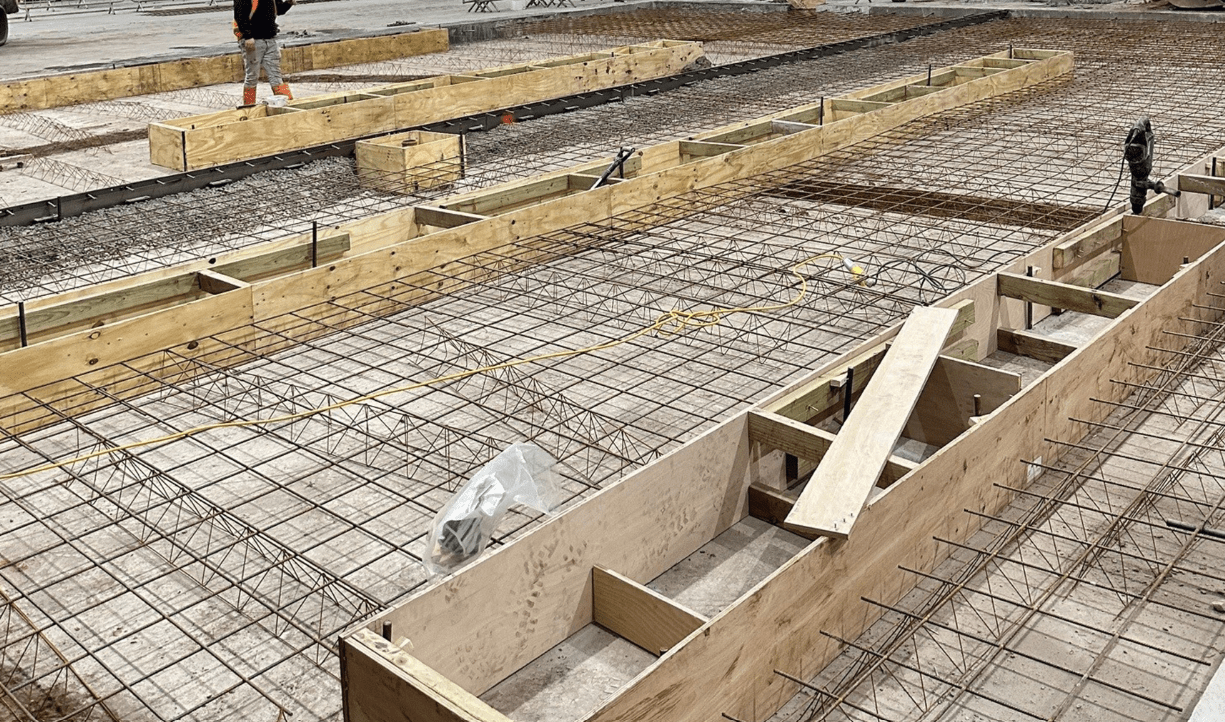
Stockton constructed new Reinforced Concrete (RC) slab to extend the existing factory footprint, and re-levelled the warehouse floor. The team built large pad foundations as the load-bearing supports for new steel columns as part of the extended building’s structural framework and installed chiller plinths installed to isolate vibrating cooling equipment from the main building structure. Advanced Damp Proof Membranes (DPM) were installed too to protect stored goods.
Outside, Stockton constructed footpaths with kerbs and path edgings, finished with a tarmacadam topping for a smooth, durable, weather-resistant finish for workforce and pedestrian access.
Health, safety and environmental compliance
Stockton Group achieved full compliance with all health and safety requirements, and received a score of 100% from an external Achilles Audit visit to site.
Do you have a civils project you’d like to talk about?
Contact Stockton Group today to chat about how we can support your next scheme.